- No.1068, Nanwan Rd, Kunshan city 215341, Jiangsu Province, P. R. China
- info@ya-va.com
- +86 18017127502
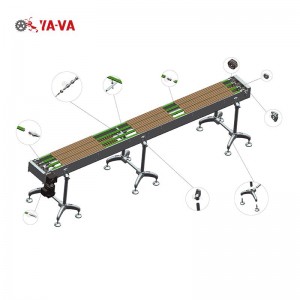
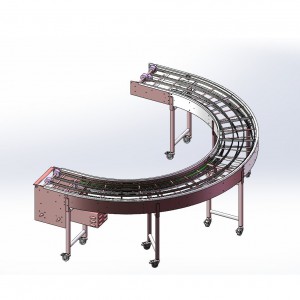
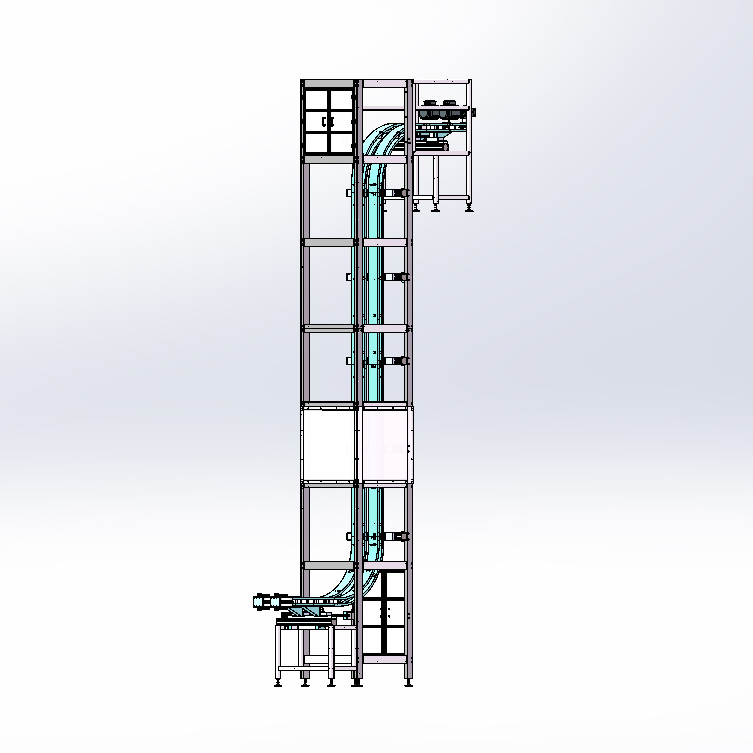
Featured Modular Conveying Solutions for Pharma Packaging
Explore our specialized module components designed for high-density container handling, precision elevation, and curved track transitions across cleanrooms and packaging facilities.
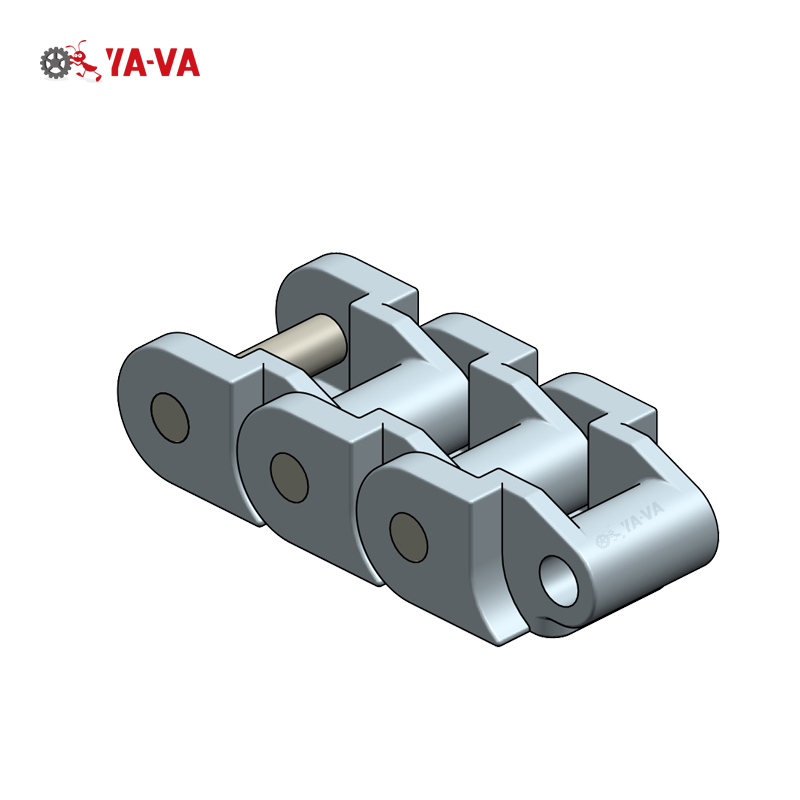
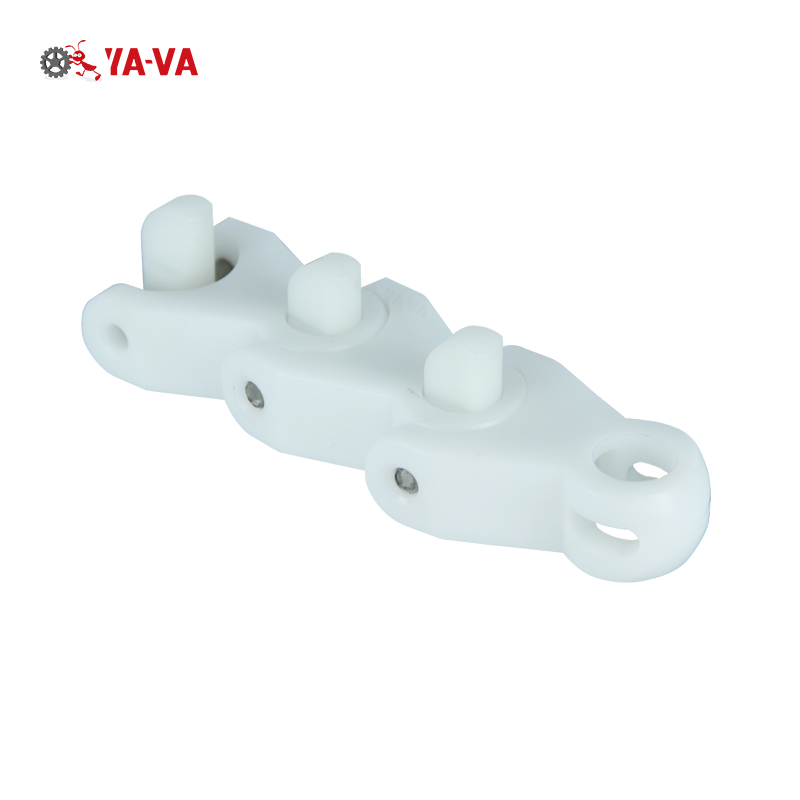
Commercial & Industrial Landscape of Modular Belts in Pharmaceuticals
The global pharmaceutical manufacturing landscape is undergoing a monumental shift toward hyper-automation, stringent biological safety, and digitized serialization. In this high-stakes production environment, the selection of material handling infrastructure—specifically the conveyor modular belt for pharmaceutical industry applications—plays a decisive role in ensuring line efficiency, zero contamination, and total regulatory compliance.
Pharmaceutical processing demands absolute reliability. Whether conveying sensitive glass vials, liquid-filled IV bags, blister packages, or secondary cartoned medicine, modular plastic conveyor belts offer significant operational superiority over traditional rubber or stainless-steel flat belts. Built from FDA-compliant thermoplastics such as Polypropylene (PP), Polyethylene (PE), and Polyacetal (POM), modular plastic belts eliminate lubricant contamination risks, resist harsh chemical cleaning protocols, and maintain dimensional stability across cleanrooms (ISO 5 to ISO 8).
FDA & GMP Compliance
Fabricated using non-toxic, food-grade materials certified under FDA 21 CFR regulations and EU 10/2011 standard guidelines. Formulated to resist microbial adhesion and prevent bio-film accumulation during continuous drug production.
Clean-In-Place (CIP) Design
Featuring open-hinge geometry and flush-grid surface profiles, modular belts facilitate rapid Clean-In-Place (CIP) and Sterilize-In-Place (SIP) routines, dramatically minimizing line turnaround times between batch changes.
Anti-Static & ESD Protection
Specialized electrostatic dissipative (ESD) polymer compounds prevent electrical charges from accumulating during rapid dry product handling, safeguarding delicate micro-electronic packaging and powder filling lines.
Deep Application Scenarios in Modern Pharmaceutical Production
Modular conveying systems are not merely transportation tracks; they serve as synchronized arterial systems integrating filling machinery, checkweighers, labeling units, and automated case packers.
1. Sterile Ampoule & Glass Vial Handling
Glass container breakage during high-speed filling causes costly downtime and severe contamination risks. Modular plastic belts with smooth, low-friction flat-top surfaces provide a stable footprint for lightweight glass vials. The intermeshed module structure dampens line vibrations, preventing tipping, scratching, or bottle-to-bottle collisions in high-speed buffer tables and rotary accumulation zones.
2. Blister Packaging & Secondary Cartoning
In high-speed thermoforming and blister sealing lines, modular belts equipped with custom flights and side walls ensure precise pitch synchronization. Products move seamlessly from primary thermoforming machines to automatic cartooning machinery with zero slipping or misalignment, supporting throughput rates exceeding 600 blister packs per minute.
3. Freeze-Drying (Lyophilization) Transfer Lines
Lyophilization processes demand clean, temperature-resistant material transfer systems. Polypropylene and custom acetal modular belts operate efficiently under extreme temperature fluctuations, carrying semi-stoppered vials into sterile freeze-drying chambers under strict laminar airflow conditions.
Technical Material Specifications
- Polypropylene (PP): Standard for chemical exposure and washdown processes; heat resistance up to 100°C.
- Polyacetal (POM): Ultra-high mechanical strength, low friction coefficient, exceptional wear resistance for heavy unit loads.
- Polyethylene (PE): Outstanding low-temperature performance down to -40°C, ideal for cold-chain storage and cryogenic processing.
- Self-Lubricating Formulations: Eliminates external liquid lubricants, keeping cleanrooms free of aerosol contaminants.
Our Strength
We are an independent company that has developed, produces and also maintains the conveyor system to ensure that our customers receive the most cost effective solutions available today.


About Us
YA-VA is a leading high-tech company providing intelligent conveyor solutions.
And it consists of Conveyor Components Business Unit; Conveyor Systems Business Unit; Overseas Business Unit (Shanghai Daoqin International Trading Co., Ltd.) and YA-VA Foshan Factory.
With over two decades of engineering excellence, YA-VA integrates state-of-the-art polymer processing, precision mold manufacturing, and automated robotics to supply pharma-grade modular conveyor belts, flexible chain conveyors, and custom handling systems worldwide.

Chain Conveyors & Flexible Slat Lines
Flexible slat chain conveyor products lines cover a wide range of applications. These multiflexing conveyor systems use plastic chains in many configurations...
Designed for multi-dimensional routing, YA-VA flexible chains can elevate, lower, twist, and turn in extremely tight footprints, making them ideal for space-constrained pharmaceutical cleanrooms and complex packing rooms.
Get in TouchFuture Development Trends: AI Integration & Smart Conveying
As the pharmaceutical industry adopts Industry 4.0 standards, modular conveyor belts are evolving from passive mechanical components into intelligent data-generating assets within the smart factory architecture.
Predictive Wear Sensors
Embedded RFID tags and IoT micro-sensors within modular belt links measure real-time pitch elongation, friction coefficient shifts, and surface wear, sending predictive maintenance alerts before line failures occur.
Dynamic Speed Synchronization
Smart modular conveyors communicate directly with vision inspection systems and serializing printers, dynamically adjusting linear speeds to optimize bottle spacing for zero-defect barcode readability.
Sustainable Bio-Polymers
Next-generation modular belts incorporate eco-friendly bio-based polymers and recyclable engineering resins, aligning with global pharmaceutical sustainability goals and reduced carbon footprints.
News and Information
Stay updated with the latest technological developments, exhibition presence, and technical guides from YA-VA Conveyors.
YA VA Looks Forward to Welcoming You in June 2026
Join our global engineering team as we unveil next-generation automated modular conveyor solutions for pharmaceutical processing.
View Details →
YA-VA Thailand Bangkok PROPAC
YA-VA Thailand Bangkok PROPACK exhibition concluded successfully two days ago. We would like to express our sincere gratitude to all our valued customers for visiting our booth. Your support is the driving force behind our progress. BOOTH NO:AY38 We sincerely inv...
View Details →What is the difference between chain and belt conveyor? How many types of conveyor chains are there?
What is the difference between chain and belt conveyor? Chain conveyors and belt conveyors are both used for material handling, but they differ in design, function, and applications: 1. Basic Structure Feature Chain Conveyor Belt Conveyor Driving Mechanism Uses...
View Details →Our Cooperative Partners
Trusted by world-class pharmaceutical brands, system integrators, and packaging machinery manufacturers worldwide.



Complete Modular Conveyor Systems Portfolio
More than 20 years focusing on transportation machinery R&D development and manufacturing, In the future Stronger and bigger in the industry scale and brand.