- No.1068, Nanwan Rd, Kunshan city 215341, Jiangsu Province, P. R. China
- info@ya-va.com
- +86 18017127502
Featured Straight Roller & Modular Conveyors for Dairy
Precision-engineered continuous conveyance systems purpose-built for milk crate accumulation, dairy carton transport, and secondary washdown packaging environments.

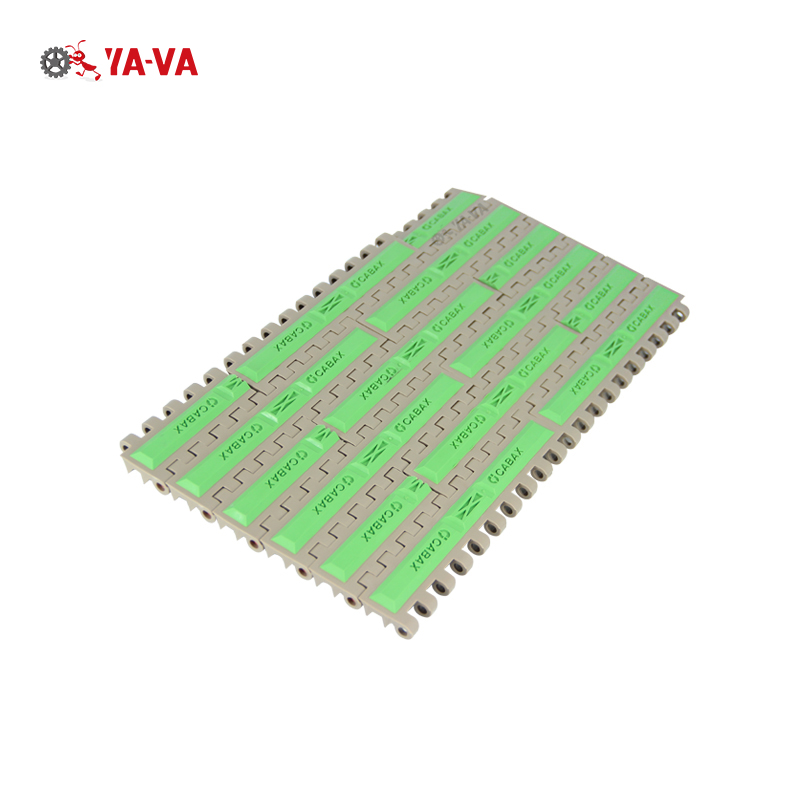
YA-VA Straight Modular Belt Conveyor for Dairy Crates
High-tensile plastic modular straight conveyance tailored for wet dairy environments, handling heavy bottle crates and secondary packaging.
Explore Details →
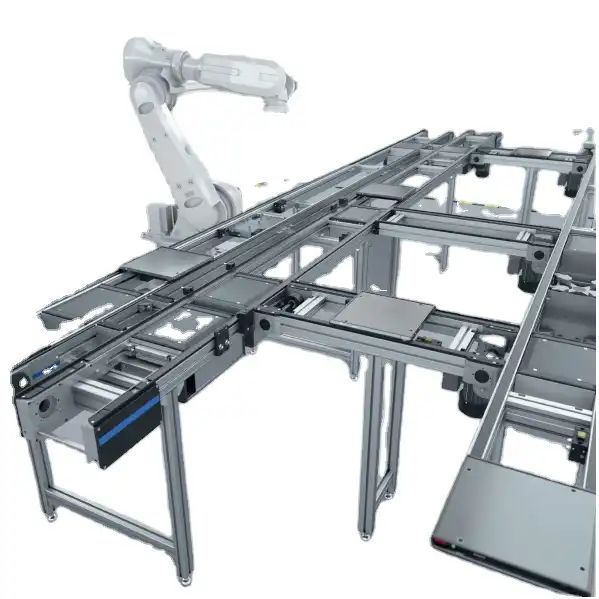
Dairy Plastic Roller Conveyor System
Corrosion-resistant plastic rollers equipped with sealed stainless bearings designed for gentle milk jug turning and low-friction conveying.
Explore Details →
Chain Driven Dairy Case Roller Conveyor
Heavy-duty motorized drive roller designed to transport heavy dairy cartons, bulk butter blocks, and cheese bulk tubs without slippage.
Explore Details →
Dairy Bottle Gripper & Straight Infeed System
Synchronized high-speed gripper and straight infeed handling for rapid elevation, invert rinsing, and orientation of yogurt & milk bottles.
Explore Details →State of Dairy Intralogistics: Why Straight Roller Conveyors Are Fundamental
From farm milk reception to ultra-clean aseptic bottling and cold-chain palletizing, modern dairy operations demand uncompromised hygiene, zero line bottlenecks, and IoT-driven reliability.
Sanitary Washdown (IP69K)
Constructed using electro-polished SUS304/SUS316 stainless steel with seamless welds, self-draining surfaces, and washdown-safe bearing cavities to eliminate bacterial pooling in dairy production zones.
Zero-Pressure Accumulation
Equipped with intelligent Motorized Drive Rollers (MDR) and photocell sensor arrays, avoiding line collisions, protecting delicate liquid cartons, and eliminating scuffing on premium gable-top milk packaging.
IoT Smart Diagnostics
Embedded thermal sensors and vibration diagnostics monitor roller bearing health in cold room environments (-25°C to +4°C), predicting maintenance needs and avoiding costly dairy line shutdowns.
1. Commercial Landscape and Market Drivers in Dairy Manufacturing
The global dairy processing industry is experiencing profound structural transformation. Accelerating consumer demand for extended shelf-life (ESL) milk, UHT pasteurized dairy beverages, Greek yogurts, plant-based milk alternatives, and artisanal cheeses requires processing facilities to operate at peak operational efficiency without compromising biological safety. Material handling systems represent the arterial backbone of this manufacturing ecosystem. Among various conveying mechanisms, the straight roller conveyor for dairy industry applications serves as the critical transit bridge connecting primary filling, secondary packing, visual inspection, case packing, and end-of-line robotic palletizing.
In modern high-speed dairy processing plants running at rates exceeding 20,000 to 45,000 units per hour, material flow must be meticulously synchronized. Any micro-stoppage caused by carton tipping, roller jamming, or bearing seizure can cause upstream aseptic fillers to pause, triggering expensive product dump cycles and extensive Clean-in-Place (CIP) re-sterilization routines. Consequently, dairy enterprise engineers and facility architects place rigorous design specifications on straight roller conveyors: they must combine absolute physical robustness, non-corrosive chemical resilience against foaming caustic wash solutions, and micro-precision motor control.
2. In-Depth Dairy Application Scenarios for Straight Roller Conveyors
Dairy manufacturing facilities are characterized by diverse atmospheric zones ranging from wet, high-humidity processing rooms to dry packaging bays and sub-zero blast freezing vaults. Straight roller conveyors must be configured precisely to match the unique mechanical, thermal, and hygiene conditions of each line stage:
Scenario A: Secondary Packaging & Case Accumulation Lines
Once liquid milk bottles, aseptic bricks, or yogurt cups are grouped and sealed inside corrugated shipping cases, shrink-wrapped bundles, or reusable plastic dairy crates, straight roller conveyors take command of product transit. Here, Motorized Drive Roller (MDR) straight conveyors provide segmented Zero-Pressure Accumulation (ZPA). Each zone operates independently, starting and stopping based on downstream optical photo-eye triggers. This prevents corrugated dairy cases from bumping together, safeguarding package aesthetics, preventing carton deformation, and ensuring tamper-evident seals remain uncompromised.
Scenario B: Wet Zone Washdown & Dairy Bottle Infeed Buffering
In blow-molding and bottle filling outfeed zones, humidity is constantly high and daily chemical sanitization is standard operating procedure. Straight roller conveyor systems configured with stainless steel shafts, food-grade UHMW-PE guide profiles, and sealed polymer roller bearings resist daily washdown with chlorinated alkaline detergents and peracetic acid sanitizers. Open-frame stainless steel side channels prevent stagnant water accumulation, ensuring that drainage is swift and complete after intensive washdown shifts.
Scenario C: Cold Chain & Cheese Aging Room Material Handling
Dairy cold chains demand materials that maintain mechanical elasticity and drive efficiency in low-temperature environments (+4°C cold storage down to -25°C blast freezers for butter blocks and ice cream hardening tunnels). Conventional conveyor rollers often fail due to lubricant solidification, brittle plastics, and condensation corrosion. Engineered straight roller conveyors utilize low-temperature synthetic lubricants, stainless steel precision bearings, and specialized polyurethane drive bands that ensure reliable friction drive transmission without cracking or slipping.
Scenario D: End-of-Line Palletizing Infeed & Inspection Reject Lines
Prior to robotic palletizing, dairy cases must undergo weight verification, barcode labeling, and vision inspection. Straight roller conveyors provide steady, vibration-free linear motion that ensures high-speed inline checkweighers and barcode scanners capture clean data without read errors. If a metal contaminant or underfilled container is flagged by inspection systems, dedicated high-speed pneumatic pop-up transfer rollers embedded inside the straight section divert the non-compliant dairy crate seamlessly into an inspection spur.
3. Advanced Engineering Specifications: Built for Modern Dairy Hygiene Standards
Meeting global hygiene standards such as EHEDG (European Hygienic Engineering & Design Group), 3-A Sanitary Standards, and FDA Food Safety Modernization Act (FSMA) compliance requires rigorous structural attention to detail. Every component of our straight roller conveyor systems reflects deep hygienic engineering:
- Hygienic Framework: Formed from 304 or 316L stainless steel with continuous sanitary welds polished to Ra ≤ 0.8 μm. Frame members feature 45-degree chamfered top edges to shed liquid run-off and prevent dust, milk residue, or moisture accumulation.
- Sanitary Roller Construction: Roller tubes are available in electro-polished stainless steel or heavy-wall food-grade polypropylene/PVC. End caps feature labyrinth seals paired with dual-contact nitrile seals that prevent the ingress of washdown water into inner bearing cavities.
- Tool-Less Component Disassembly: Fast-release roller axles and tool-free quick-release side guides allow sanitation crews to remove rollers within minutes for deep ultrasonic chemical sanitization, reducing plant sanitation cycle times by up to 35%.
- Intelligent 24V/48V Brushless DC Drives: Decentralized drive rollers eliminate dangerous central drive shafts, external oil-filled gearmotors, and grease-lubricated sprockets from open food zones, completely eliminating hydrocarbon contamination hazards.
4. Future Development Trends: Industry 4.0, Digital Twins & Sustainable Dairy Operations
The convergence of industrial automation and edge computing is reshaping dairy conveyance. Future-ready straight roller conveyor installations now feature interconnected smart sensors that communicate via Ethernet/IP, PROFINET, or IO-Link networks directly to the plant's MES/SCADA system. Real-time condition monitoring tracks roller rotational resistance, drive amperage, and motor temperature. When bearing degradation is detected before an outright mechanical failure, predictive maintenance alerts notify maintenance technicians during scheduled downtime windows, preventing catastrophic mid-shift outages.
Furthermore, sustainability is a major priority for dairy brand owners seeking carbon neutrality. Low-voltage MDR straight roller conveyors utilize "run-on-demand" logic, whereby idle conveyor sections automatically enter sleep mode when no dairy cartons are present. This operational architecture reduces plant electric power consumption by up to 60% compared to traditional continuous-run AC motor-driven conveyors, while substantially decreasing acoustic noise levels across packaging floors.
Our Strength
We are an independent company that has developed, produces and also maintains the conveyor system to ensure that our customers receive the most cost effective solutions available today.


About Us
YA-VA is a leading high-tech company providing intelligent conveyor solutions.
And it consists of Conveyor Components Business Unit; Conveyor Systems Business Unit; Overseas Business Unit (Shanghai Daoqin International Trading Co., Ltd.) and YA-VA Foshan Factory.
Over two decades of dedication to dairy, food, and beverage intralogistics enable us to engineer sanitary conveying systems that seamlessly integrate into high-speed bottling, cartooning, and automated storage operations worldwide.
Chain Conveyors & Straight Modular Line Integration
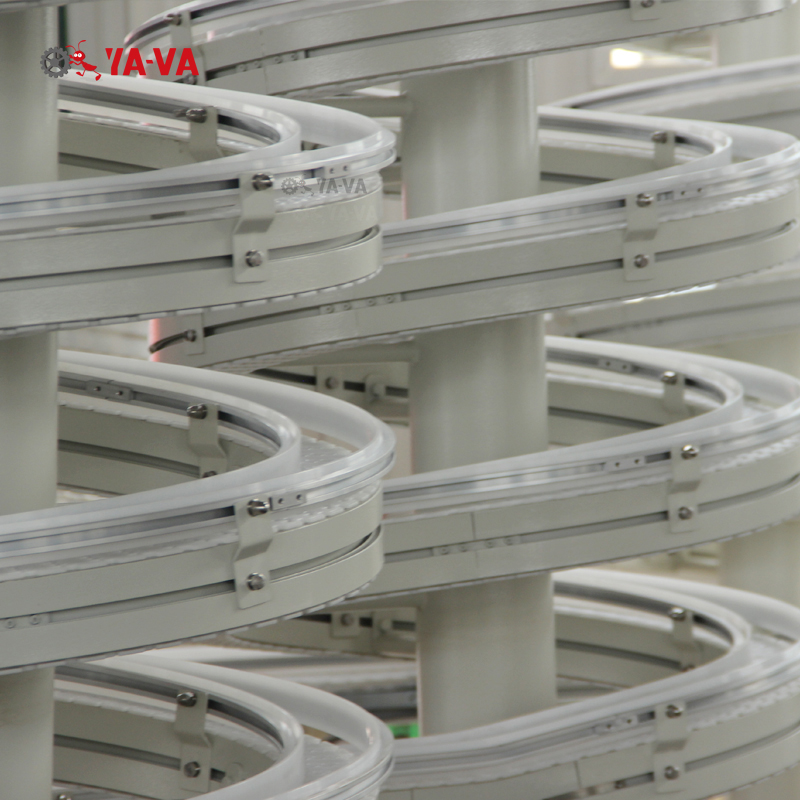
Flexible slat chain conveyor product lines cover a wide range of applications. These multiflexing conveyor systems use plastic chains in many configurations to handle milk cartons, cheese packages, and aseptic pouches with exceptional precision.
Complementing our straight roller conveyor modules, our high-performance chain conveyors facilitate seamless elevation changes, tight curves, and high-speed sortation across sanitary dairy plants.

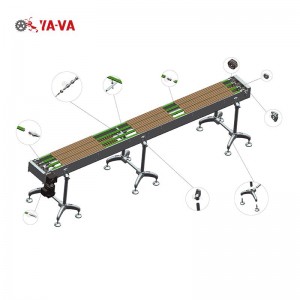
Feature Products
More than 20 years focusing on transportation machinery R&D development and manufacturing. In the future stronger and bigger in the industry scale and brand.


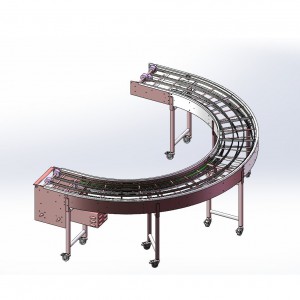
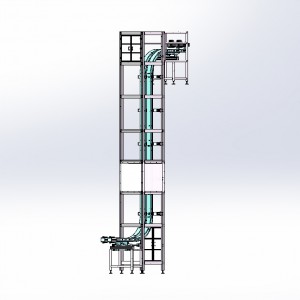
News and Information
Stay updated with the latest technological developments, exhibition appearances, and industry knowledge from YA-VA.
YA VA Looks Forward to Welcoming You in June 2026
Join us as we unveil our latest smart conveyor architectures and hygienic conveying innovations designed for food and dairy automation.
View Details →
YA-VA Thailand Bangkok PROPAC
YA-VA Thailand Bangkok PROPACK exhibition concluded successfully two days ago. We would like to express our sincere gratitude to all our valued customers for visiting our booth. BOOTH NO: AY38.
View Details →What is the difference between chain and belt conveyor? How many types of conveyor chains are there?
Chain conveyors and belt conveyors are both used for material handling, but they differ in design, function, and applications including driving mechanisms and load profiles.
View Details →Our Cooperative Partners
Partnering with world-class manufacturers in dairy, food processing, beverage bottling, and automated packaging.



Dairy Conveyance Systems & Spare Components
Explore our full line of specialized conveyor belts, chains, guide profiles, and modular structural parts supporting uninterrupted dairy line operations.